CNC Machining of Aluminium Heat Sinks and Thermal Housings
We machine aluminium heat sinks and thermal housings — dense fin arrays, flat mounting bases, recessed cavities and drilled or tapped fixing features — to your drawing. Fins may start from extruded profile or from solid billet; we finish the interfaces, bores and cavities that determine how the part fits and performs. Material, finish and inspection scope are confirmed against your print and the supplied grade.
Liquid-cooled designs follow the same machining logic but carry a different set of risks: sealing faces, burr-free passages and leak testing. We cover those under cold plates and coolant manifolds for data centres.
Flat interfaces, clean fins
Flat base, clean interfaces
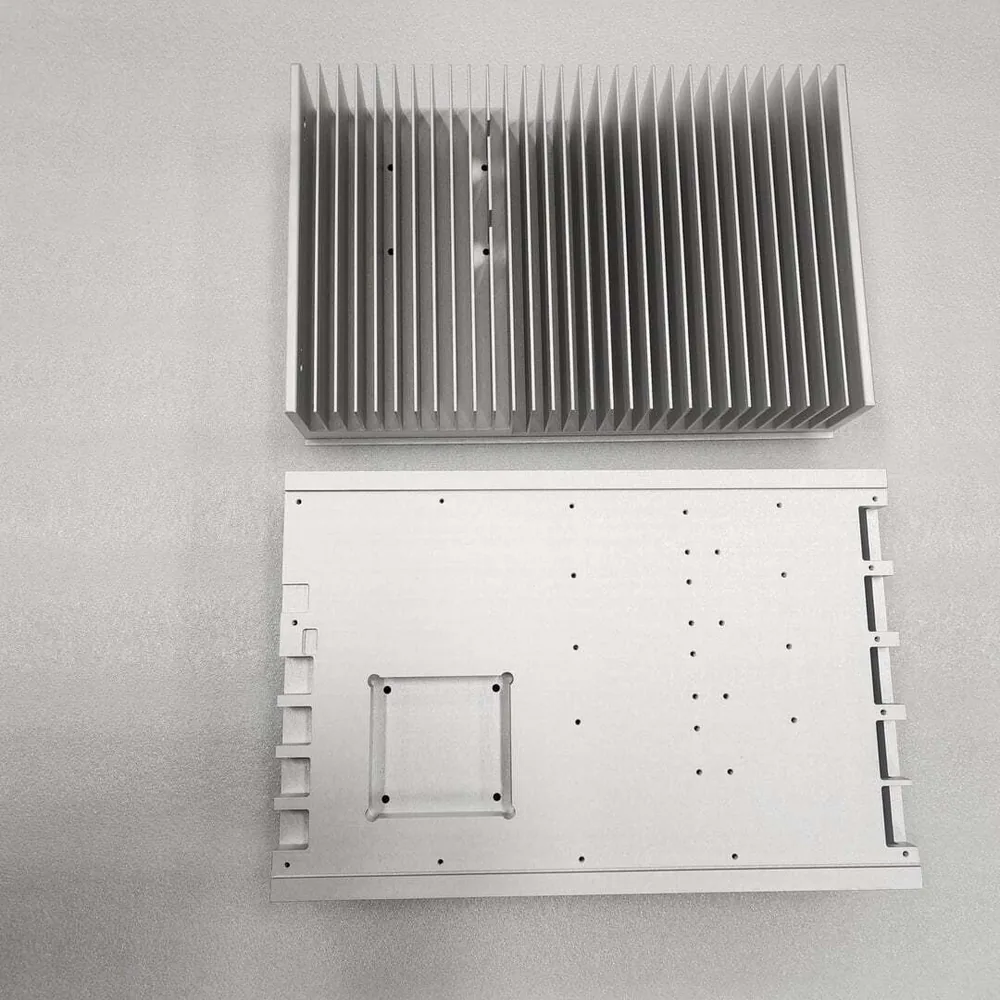
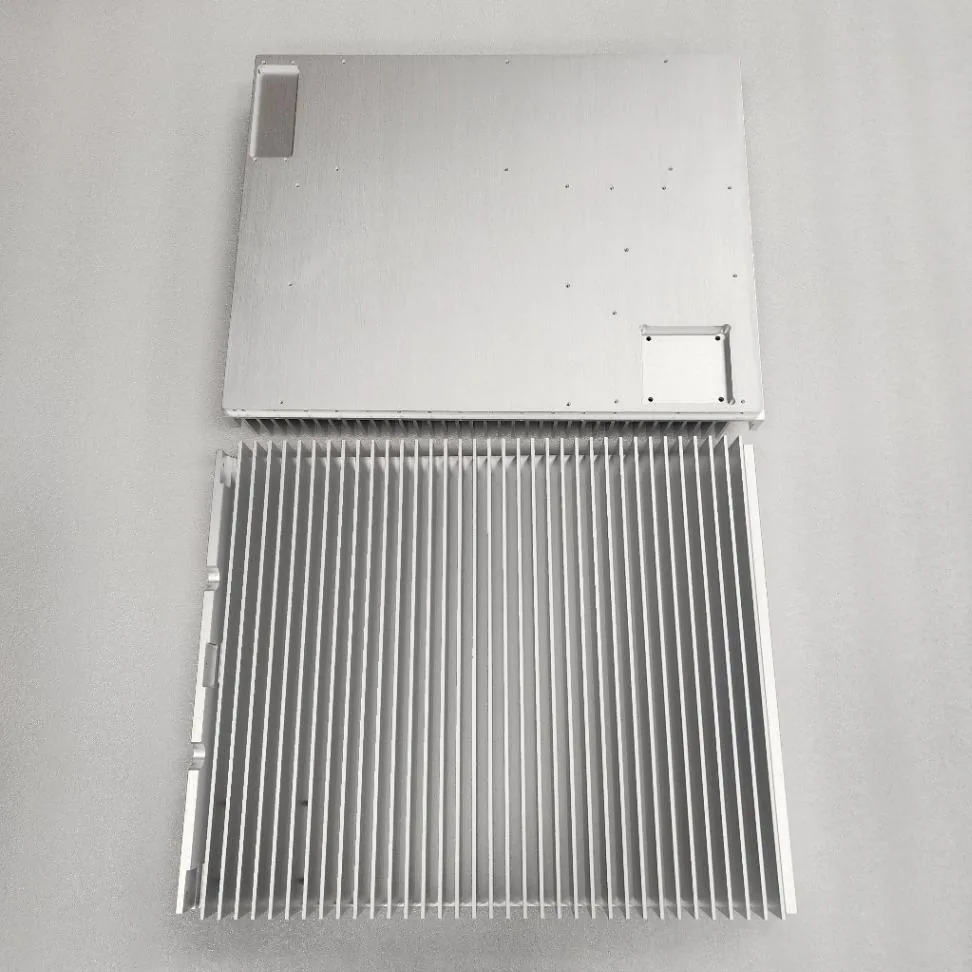
A heat sink only works if its mounting face sits flat; we machine and inspect the interface faces, not just the visible fins.
Fins without breakout
Fine fins and thin walls need controlled tooling and support to avoid chatter and burrs at the fin roots.
Cavities and fixing features to print
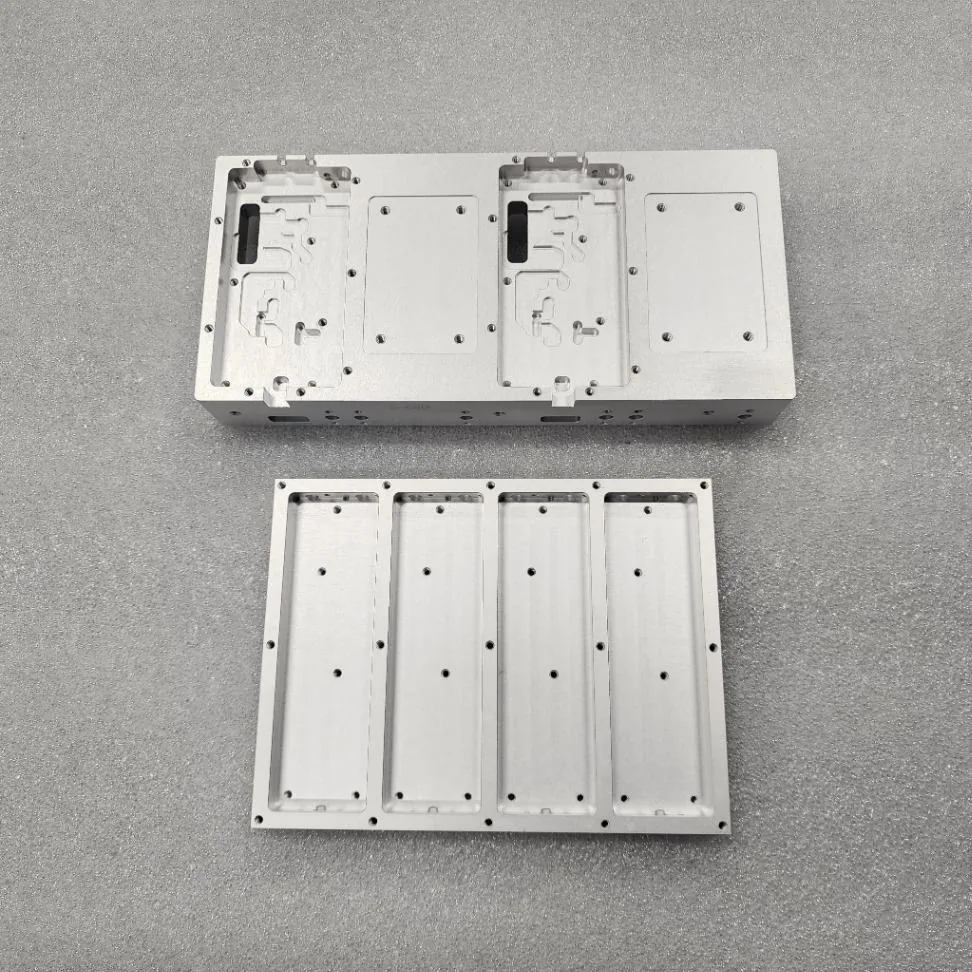
Recessed pockets, tapped holes and locating tabs are machined to the drawing and verified on the CMM.
Heat Sink Machining
What we confirm before cutting — grade-, profile- and finish-specific values come from your drawing and data sheet.
| Capability | Specification |
|---|---|
| Materials | Aluminium grades per your drawing; other thermal alloys quoted on request |
| Typical tolerance | ±0.005 mm on 5-axis work, confirmed against your drawing |
| Processes | CNC milling, facing, pocketing, drilling, tapping, countersinking, deburring |
| Milling envelope | Up to 2000 × 1000 mm |
| Features | Fin arrays · flat mounting bases · recessed cavities · through and tapped holes · locating tabs |
| Surface finish | Down to Ra 0.2 µm on metals, confirmed per feature |
| Fin stock | Extruded profile or solid billet, per your drawing — extrusion arranged with qualified partners where required |
| Surface treatment | Anodising and other finishes placed with qualified subcontractors; quality and delivery remain our responsibility |
| Inspection | Zeiss CMM on critical features; first-article inspection report on request |
| Prototype lead time | Typically 5–10 working days |
Heat sinks we have machined
Heat sinks and thermal housings from our workshop — described by what is in the photograph, not by customer or project name.
From Drawing to Delivered Part
A transparent, engineering-led process for thermal components.
Submit & Review
Send the drawing, the aluminium grade and any flatness or finish requirement. Our engineers check tool access to fin roots, datum faces and tolerances before cutting.
Quote & Material Plan
You receive a transparent quote and the route for the fin stock — extruded profile or solid billet — with inspection and any surface treatment included.
Machine & Inspect
Controlled tooling for fine fins, then Zeiss CMM inspection on interface faces and critical features, with first-article reporting.
Deliver & Support
Parts packed to protect fin tips, labelled to your drawing, with engineering support for repeat orders and revisions.
Frequently asked questions
Request a Quote
Tell us about your program. The fields below help our engineering team prioritize recurring, long-term supply programs with equipment manufacturers.
What happens after you send your files
- Within 1 business day an engineer — not a salesperson — reviews your drawings and replies.
- DFM review: tolerances, material and risk flags, before any cutting begins.
- Your quote includes a material-verification plan: grade, EN/DIN check, certificate strategy.
Critical features are verified in house · material chemistry confirmed by spectrometer · EN 10204 3.1 certificates available.
Prefer email? Write to us directly at info@prototech-machining.com
Drawings and CAD files are used only to quote and manufacture your parts. They are not shared with third parties, and we sign an NDA on request — even before you send anything.
Our form captures production type, annual quantity and project status up front — so we can focus engineering resources on long-term supply relationships, not one-off inquiries.
Talk to our team about special materials, tolerances or a failed-supplier recovery before you send drawings.